Skyeaglee Explosion-Proof CO Analyzer
2026-09-30
Pre-Holiday Production Rush: Delivering Reliable CO Gas Analyzers
Inside the Industrial Gas Analyzer Factory
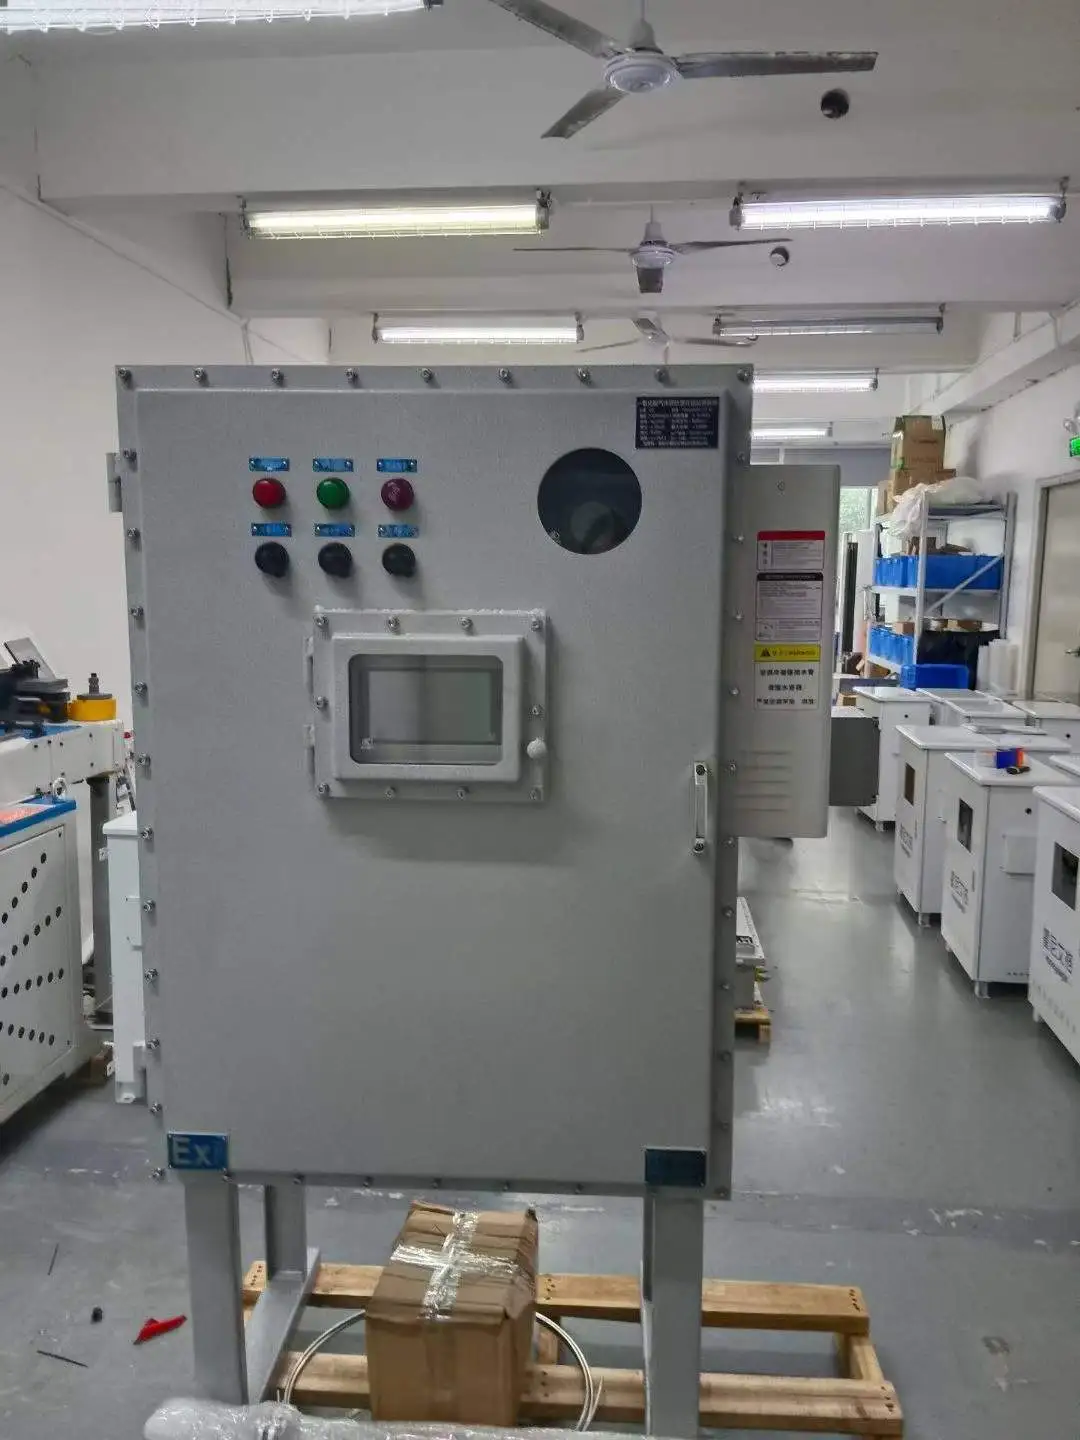
In our core manufacturing workshop, precision meets heavy-duty engineering. The image above showcases a fully assembled, explosion-proof Carbon Monoxide (CO) online detection and analysis cabinet. Resting securely on a wooden pallet in the final assembly area, this specialized system is undergoing its last rigorous quality checks. As a professional Gas Detector Manufacturer, we ensure that every unit, especially heavy-duty cabinets designed for harsh industrial environments, is physically and technically flawless before it ever reaches the shipping dock.
Commitment as a Reliable Gas Sensor Supplier
Meeting industrial safety demands means not only building rugged equipment but also ensuring it arrives on schedule. During our recent pre-holiday production rush, our Industrial Gas Analyzer Factory successfully packed and loaded a massive batch of equipment. This highlights our core operational strengths:
1. Strict Final Testing and Quality Control
Before any Gas Detection System Delivery is authorized, units like the CO analyzer cabinet are fully activated and calibrated. Our testing area verifies the explosion-proof integrity (Ex standards) and the CO sensor accuracy to guarantee 100% reliability for our B2B clients.
2. Efficient Packaging and Global Dispatch
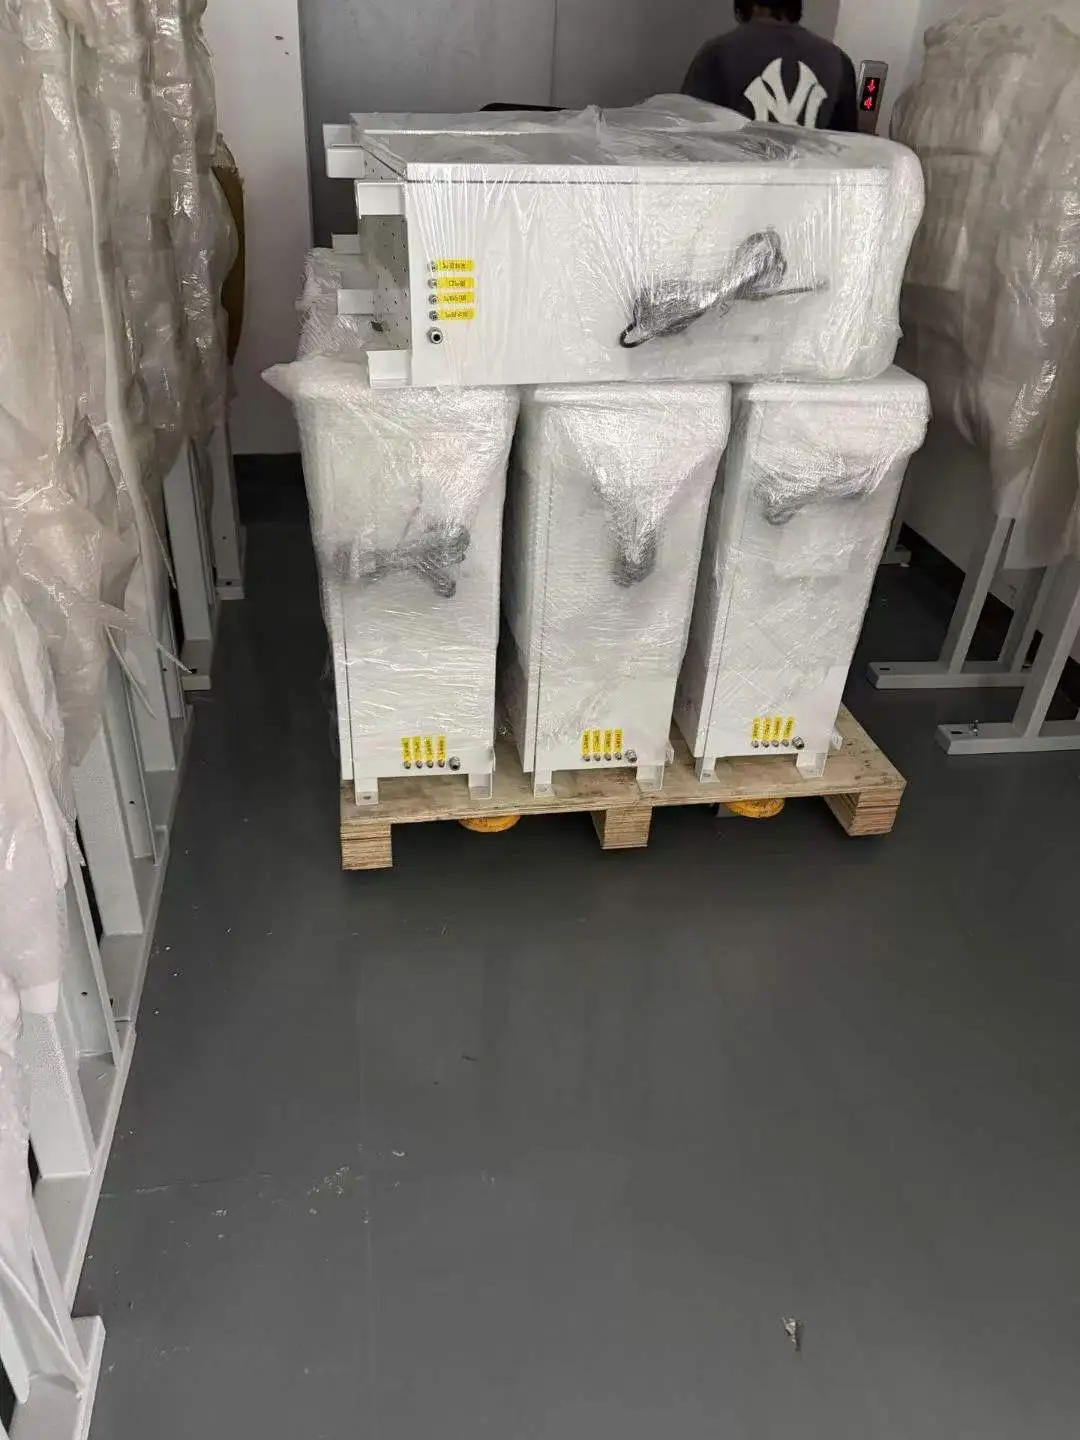
To fulfill every order without compromising quality, our logistics team executes highly organized packaging. As seen in the image above, large equipment is firmly secured onto robust wooden pallets and thoroughly wrapped to prevent any moisture or transit damage.
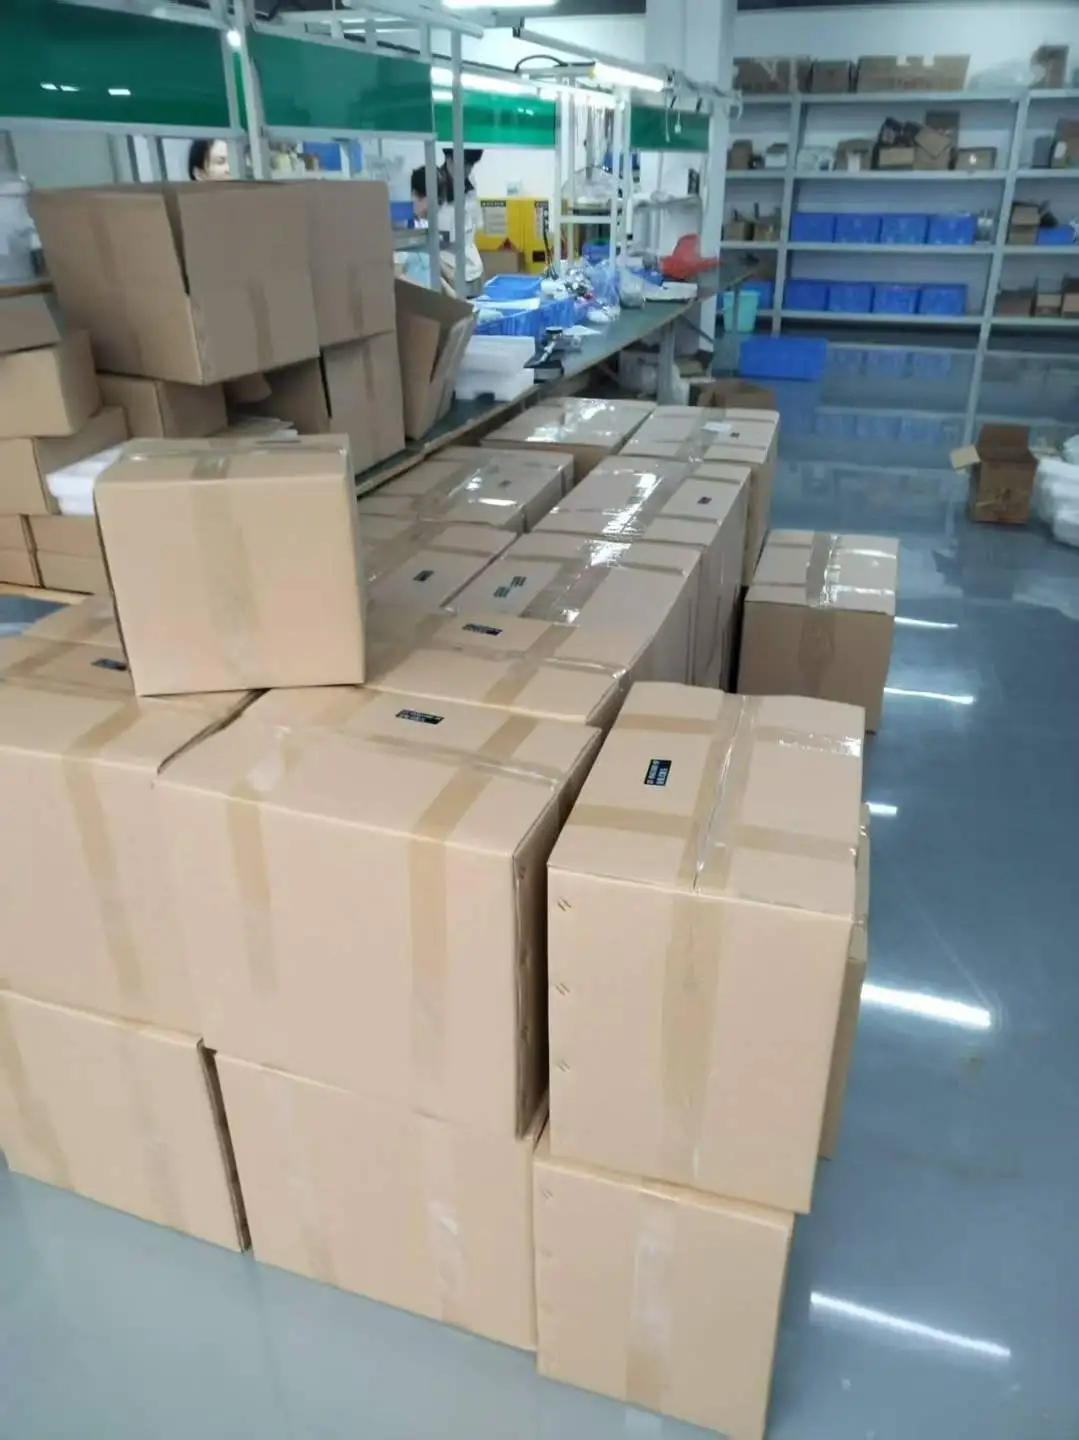
Meanwhile, standard detectors are carefully packed into uniform, reinforced cardboard boxes, stacked neatly in our dispatch zone. This meticulous attention to detail ensures that whether it's a massive analyzer cabinet or a batch of portable units, every product leaves our facility in pristine condition.
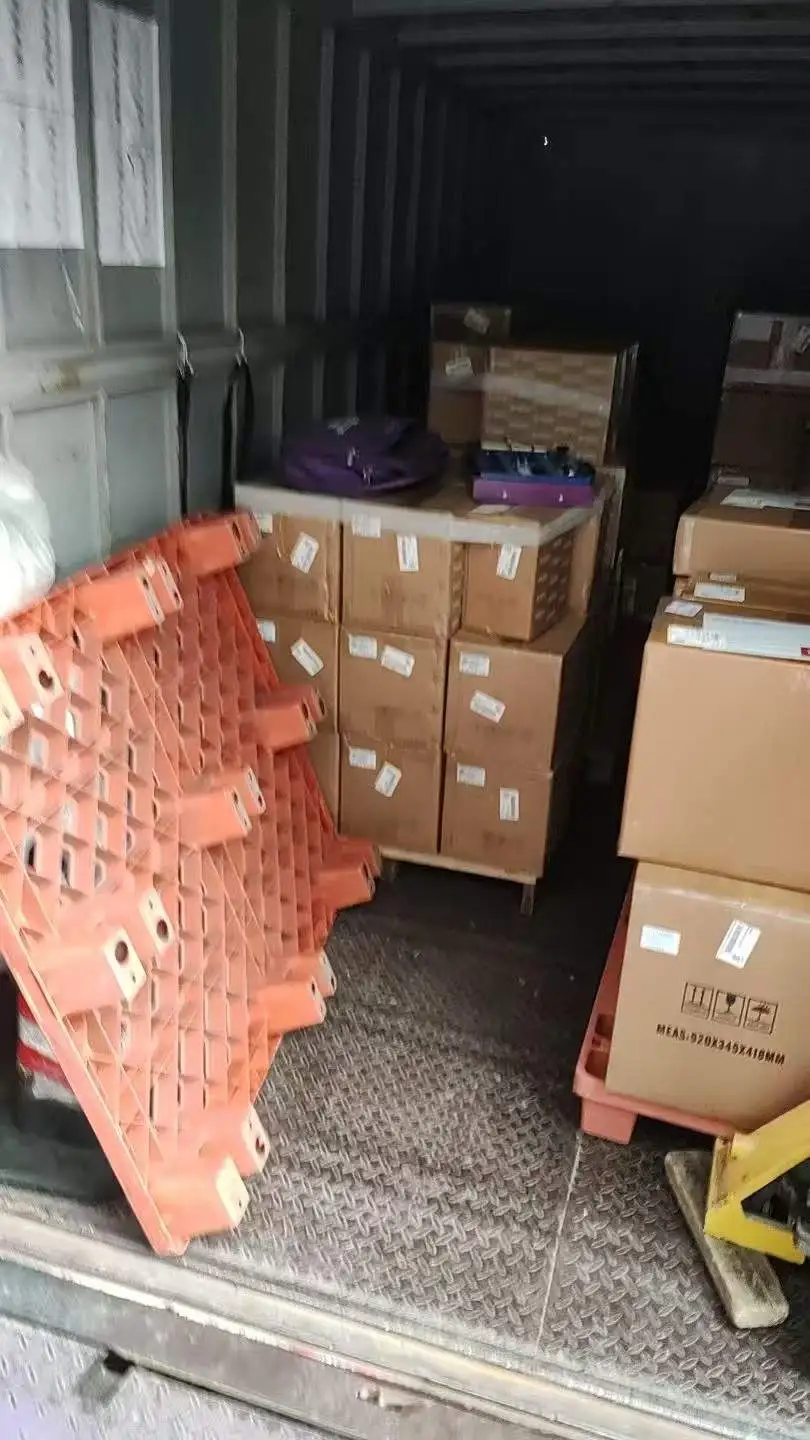
Finally, all securely packed goods are systematically loaded into shipping containers, maximizing space while ensuring stability during global transport. This pre-holiday dispatch demonstrates our capacity to handle large-scale shipments efficiently, proving that we never betray the trust our clients place in us.
Previous: No more data
Related News
Contact Us


Fill out the form