Fixed CO Preprocessing Online Monitoring System
-
Model: HNAG1000-CO
-
Detection: CO
-
Detection Principle: Electrochemical, infrared NDIR
-
Detection range: 0-500ppm, 0-10000ppm, 0-5%Vol, 0-10%VOL
Product Description
High-Precision Fixed CO Preprocessing Online Monitoring System
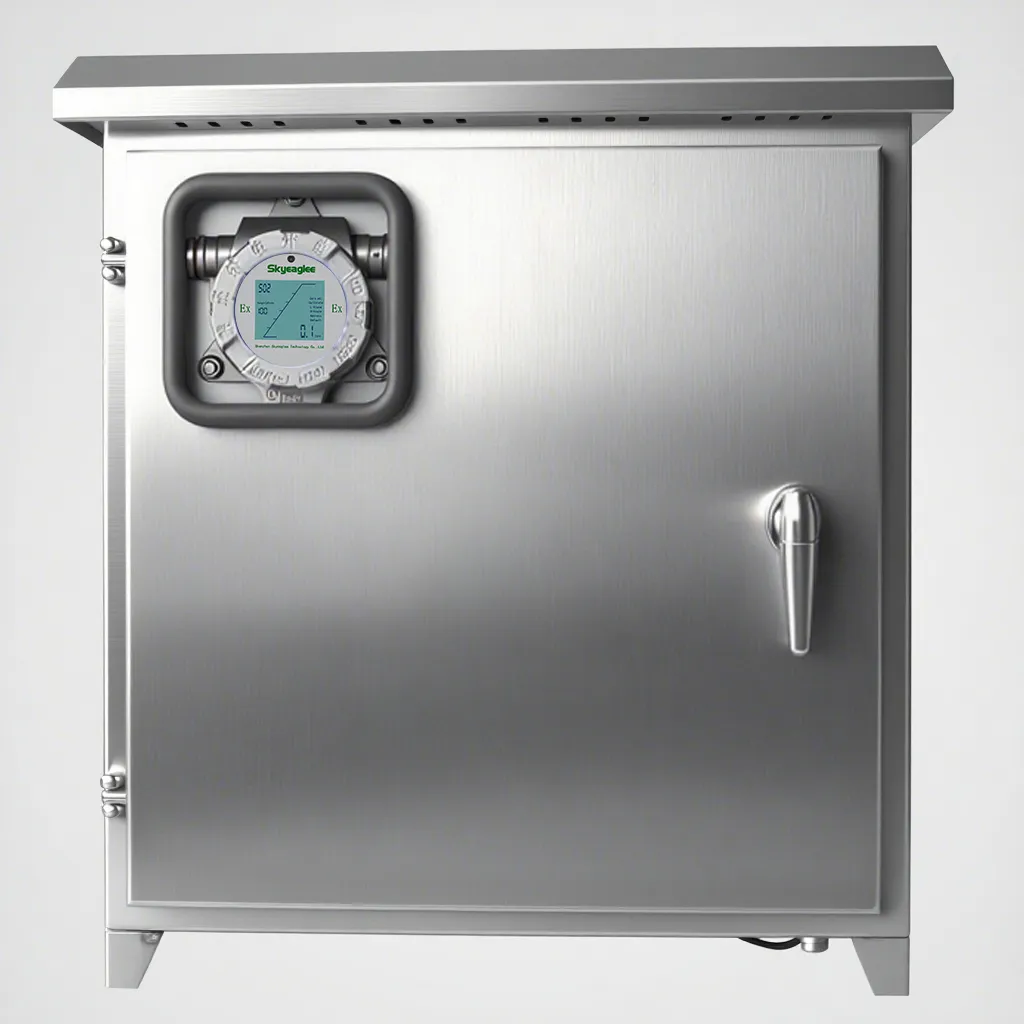
The HNAG1000 Fixed CO Preprocessing Online Monitoring System is engineered for continuous, accurate detection of carbon monoxide (CO) concentration and leakage across challenging industrial settings. By integrating high-performance electrochemical and infrared NDIR sensors with advanced microcontroller technology, this system delivers rapid response speeds (T90 < 10s), exceptional stability, and high repeatability. Its flameproof, explosion-proof wiring ensures safe deployment in hazardous zones, providing direct compatibility with user computers, control alarms, PLCs, and DCS platforms.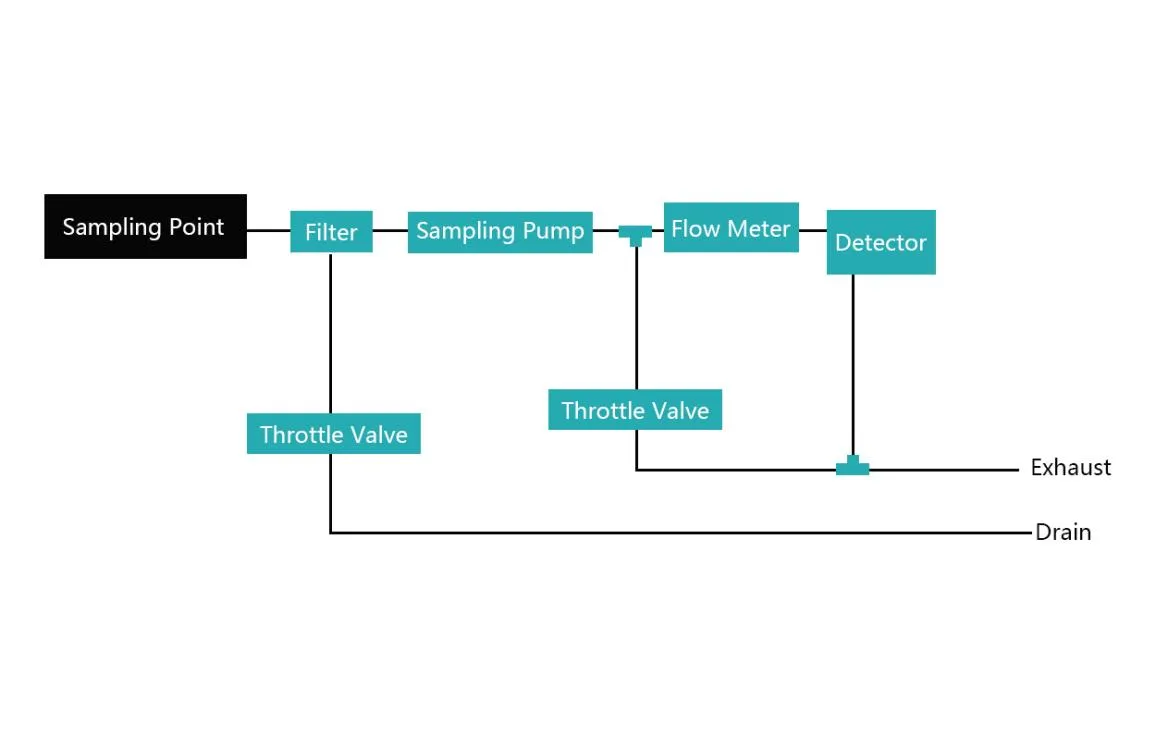
Robust Stainless Steel Enclosure & Gas Sampling Process
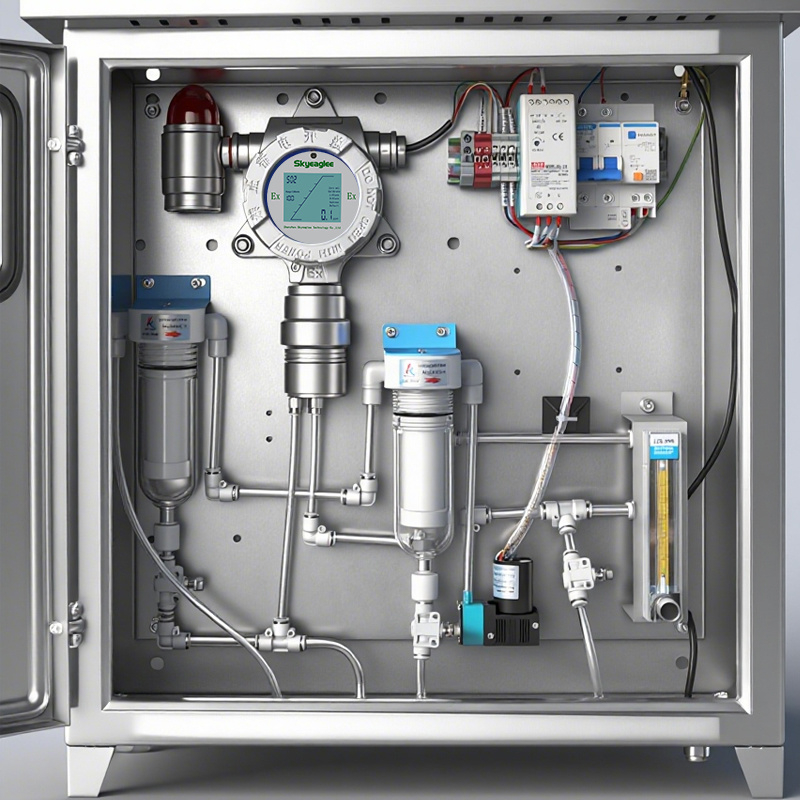
Encased in an industrial-grade stainless steel cabinet, this online monitoring system withstands corrosive and demanding ambient conditions. The integrated sampling mechanism operates with high precision: sampled gas is first drawn through a high-efficiency filter to eliminate particulate dust and impurities. A specialized sampling pump then directs the sample through an adjustable flowmeter calibrated between 0.3 and 0.5 L/min, ensuring constant pressure and stabilized gas delivery to the internal detection chamber.
Technical Specifications of Fixed Carbon Monoxide Monitor
| Parameter | Technical Specification |
| Monitored Gas |
Carbon Monoxide (CO) |
| Sensor Principles |
Electrochemical, Infrared NDIR |
| Measurement Ranges |
0-500ppm, 0-10000ppm, 0-5%Vol, 0-10%VOL |
| Resolution |
1ppm, 0.01%VOL |
| Sampling Accuracy |
±3% F.S. |
| Response Time |
T90 < 10s |
| Standard Signal Output |
4-20mA (12-bit precision, 1km), RS485 (MODBUS RTU, 1km), Relays (220VAC 3A / 24VDC 3A) |
| Optional Signal Output |
Voltage (0.4-2V, 0-5V, 0-10V), Wireless (GPRS, 4G, WIFI, LORA, ZigBee) |
| Operating Conditions |
Temperature: -20 ~ 50℃; Humidity: 0-95%RH |
| Sampling Parameters |
Temperature:≤ 120℃; Max distance: 80m (Recommended ≤ 20m) |
| Power Supply |
220V AC |
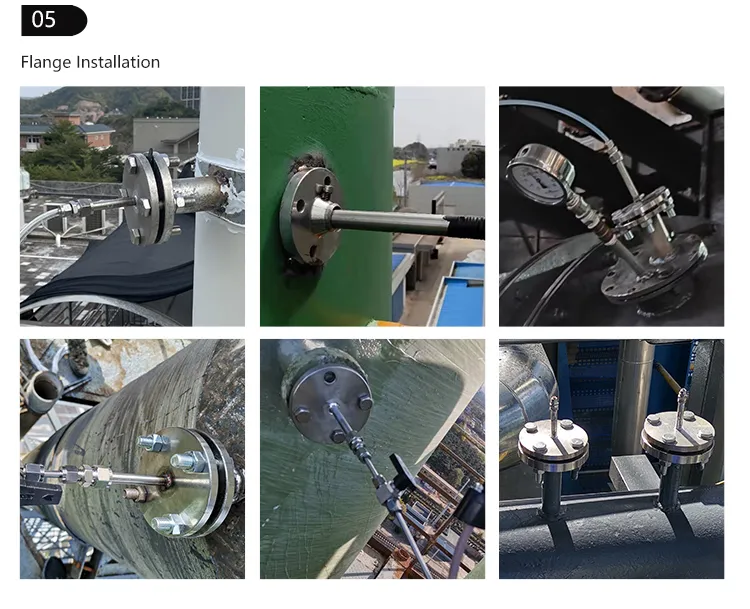
Industrial Applications & Flange Installation
The system supports standard pipeline flange installations and wall-mounted setups, providing reliable safety monitoring in critical sectors including petroleum and petrochemical refineries, chemical processing plants, steel mills, boiler rooms, thermal power stations, underground utility tunnels, and industrial process control facilities.
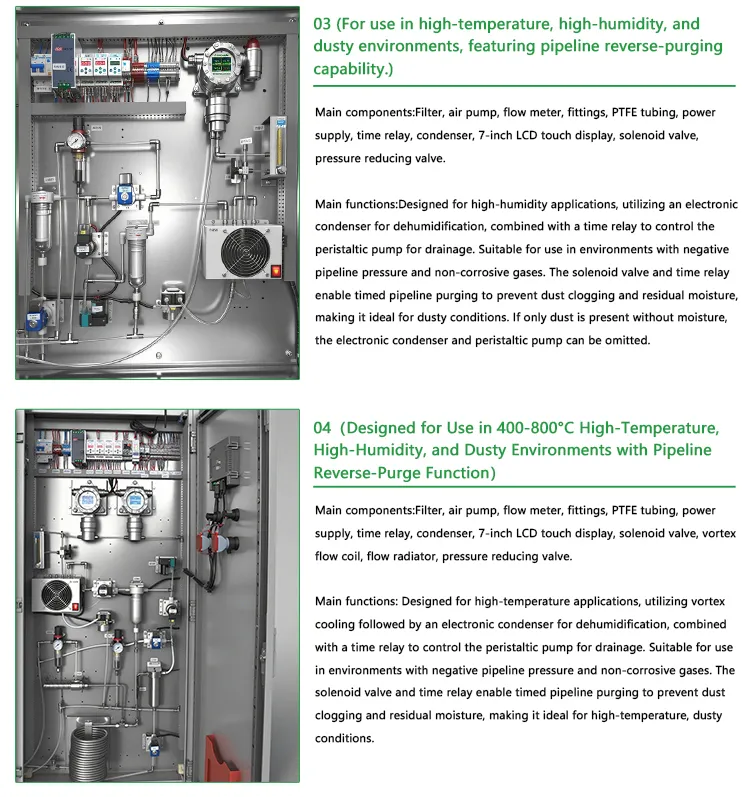
Customized Gas Pretreatment Configurations
To accommodate extreme industrial environments, multiple tailored internal configurations are available:
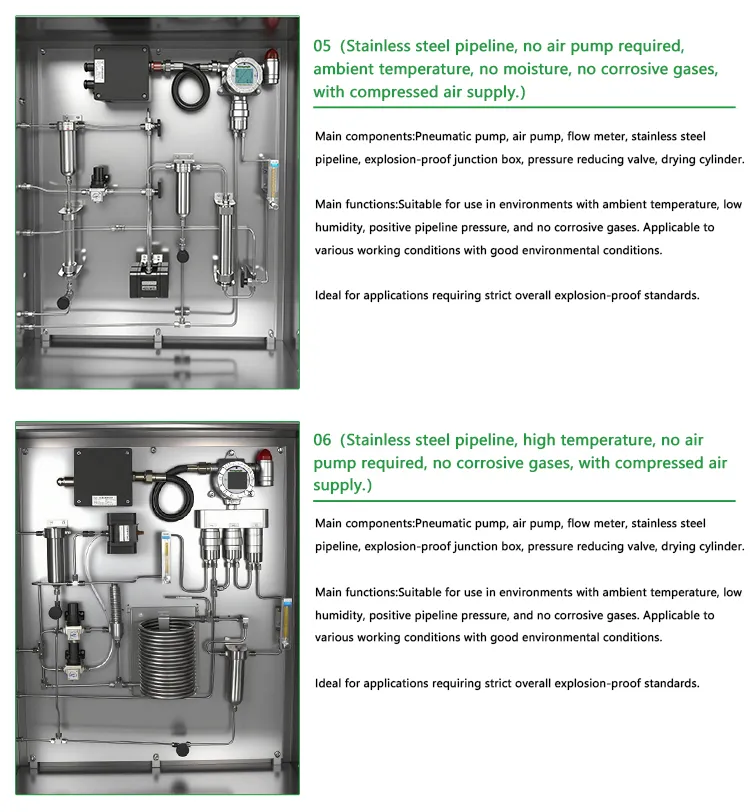
Normal to Medium Temperatures: Systems equipped with electronic condensation units and timed peristaltic drainage pumps for negative-pressure pipelines and moisture extraction.
High-Temperature & Dusty Flue Gases (400-800°C): Configurations featuring vortex cooling coils, dual filtration, and automatic time-relay reverse-purging valves to prevent sampling clogging.
High Explosion-Proof Requirements: Systems built with stainless steel pipelines and pneumatic pumps driven by plant compressed air.
Multi-Point Centralized Monitoring: Integrated multi-channel enclosures capable of monitoring multiple sampling points simultaneously.
Frequently Asked Questions (FAQ)
Q: What is the typical lifespan of the CO sensor and consumables?
A: The carbon monoxide sensor has an operational service life of approximately 1 to 3 years depending on target gas exposure and ambient conditions. The internal filter element typically requires replacement every 3 months (indicated by internal chip color alteration), while the sampling pump is rated for approximately 1 year of continuous operation.
Q: How does the system handle multi-level alarm signaling?
A: Standard units come configured with two-level threshold alarms, with an optional three-level alarm structure. Alerts trigger on-site audio-visual sound and light beacons, remote controller indicators, passive relay switch closures for ventilation activation, and automated event notifications in connected computer control systems.
Q: What sampling distance can this preprocessing monitor support?
A: The system supports an extraction sampling distance of up to 80 meters, with an optimal recommended operating distance within 20 meters to maintain sample integrity and rapid response times.
Product Recommendation
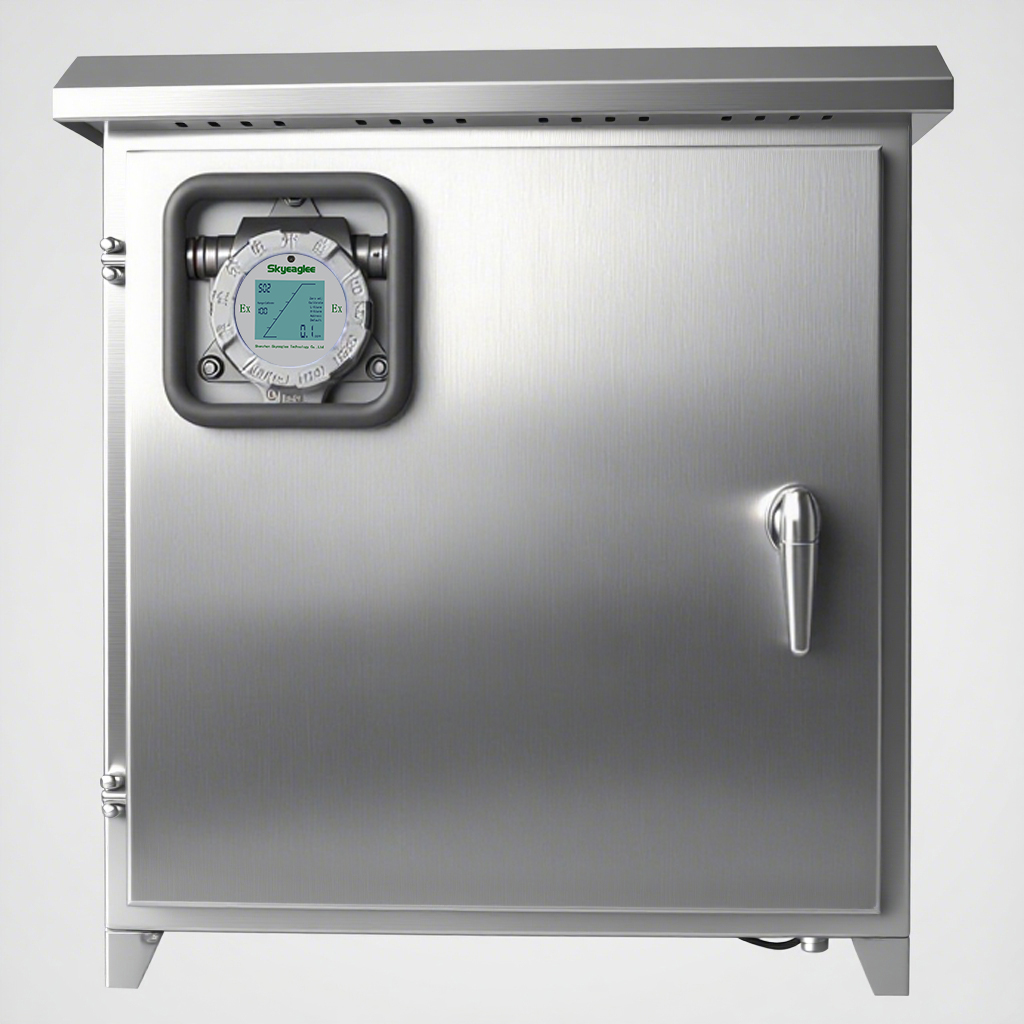
Fixed CO Preprocessing Online Monitoring System-Fixed CO Preprocessing Online Monitoring System
HNAG1000 Fixed CO Preprocessing Monitoring System provides continuous carbon monoxide detection in harsh areas. Built with advanced NDIR sensors and a rugged stainless steel enclosure, it guarantees rapid response, high accuracy, and industrial safety.
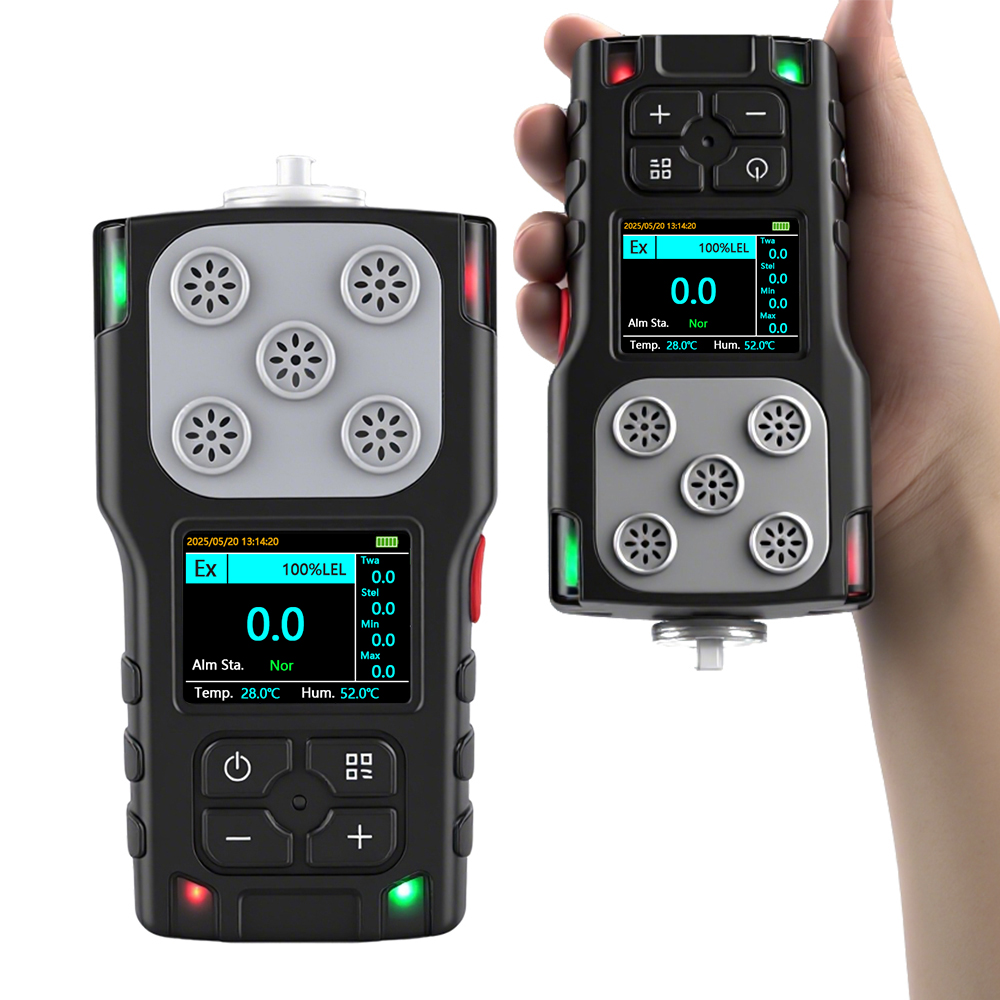
HNAG920 Portable NH3 Ammonia Single Gas Detector with Custom Ranges-HNAG920 Portable NH3 Ammonia Single Gas Detector with Custom Ranges
This HNAG920-NH3 handheld single ammonia gas detector provides 12 optional NH3 measuring ranges from 0-10ppm up to 0-100%Vol. It supports auto 180° screen rotation, 4G/WiFi/Bluetooth/LORA wireless transmission, Type-C rechargeable design, 4-side LED alarm lights, durable PC+TPU housing, and allows mobile data viewing & Bluetooth printing for chemical plants, livestock farms and refrigeration workshop hazardous gas monitoring.
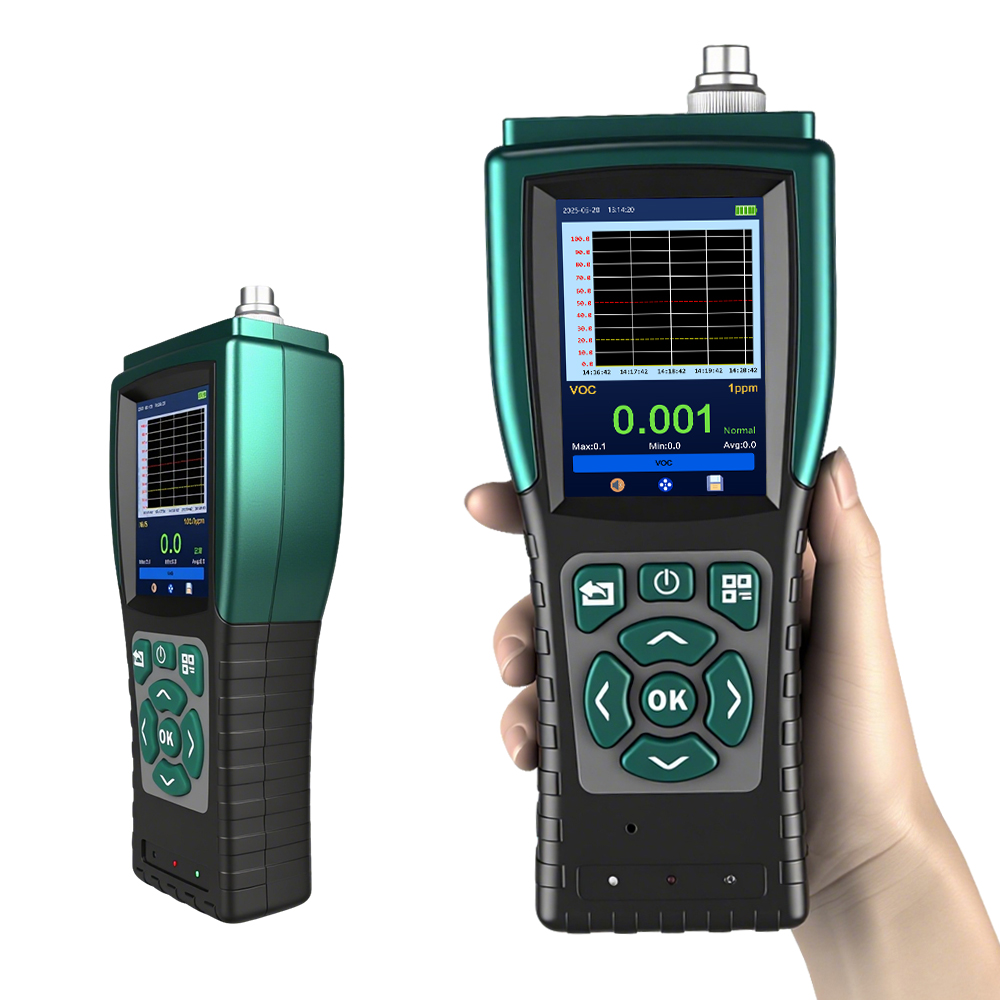
Portable Methane Gas Detector Handheld Methane Monitor-HNAG900Portable Methane Gas Detector Handheld Methane Monitor
Skyeaglee HANG-900-CH4-C portable methane gas detector with catalytic detection 0-100%LEL, IP65, Ex ib II CT4 Gb. Expandable to 6 gases, 5400mAh, USB data export. Professional methane gas monitor for oil, coal, petrochemical.
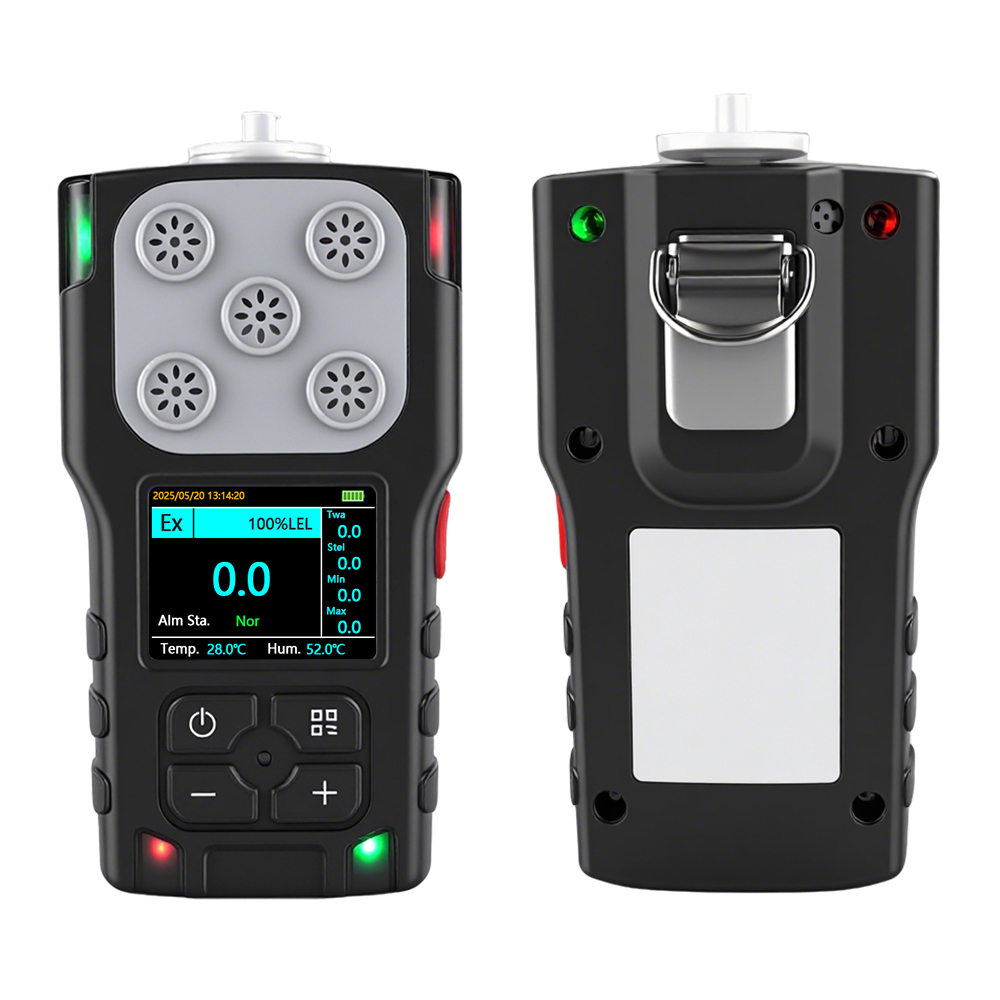
Portable pump-assisted diffusion-type hydrogen gas detector-HNAG920-H2Portable pump-assisted diffusion-type hydrogen gas detector
Explore the Portable pump - assisted diffusion - type hydrogen gas detector. This detector combines pump - assisted and diffusion - type features, offering high - precision hydrogen detection.
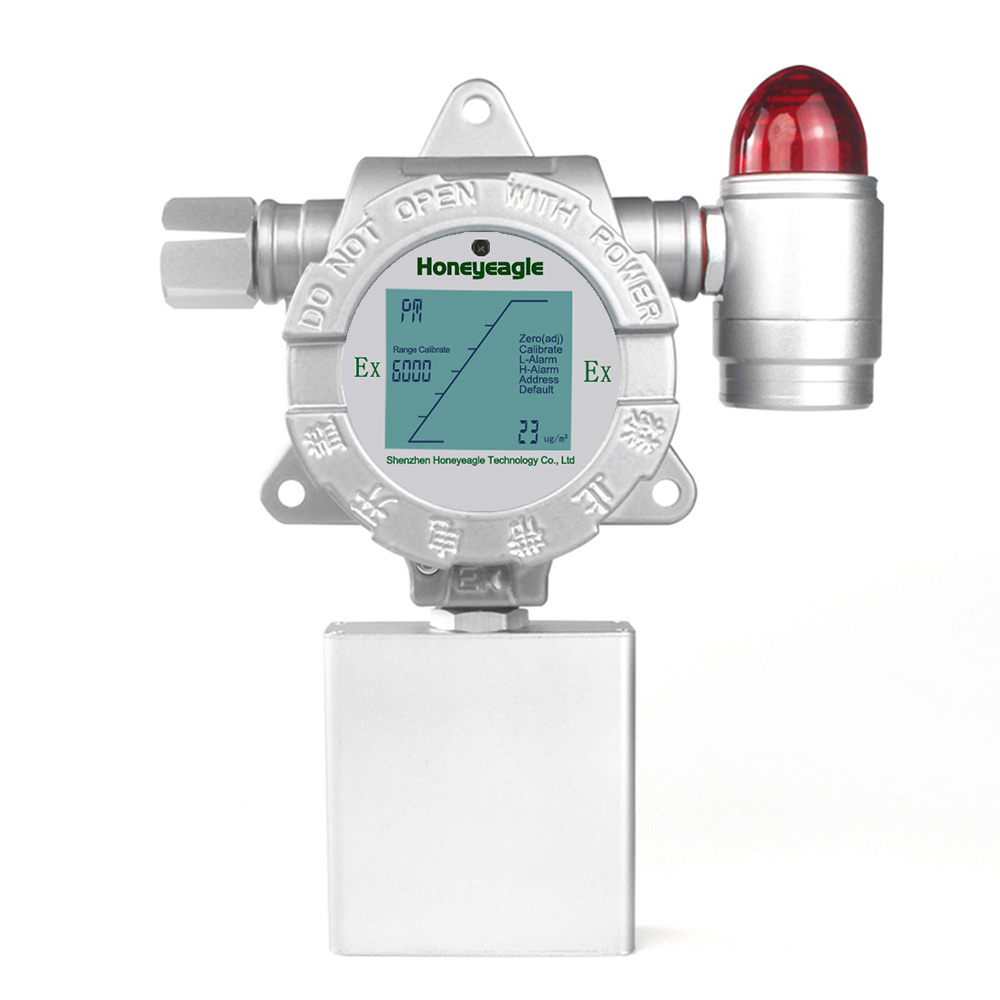
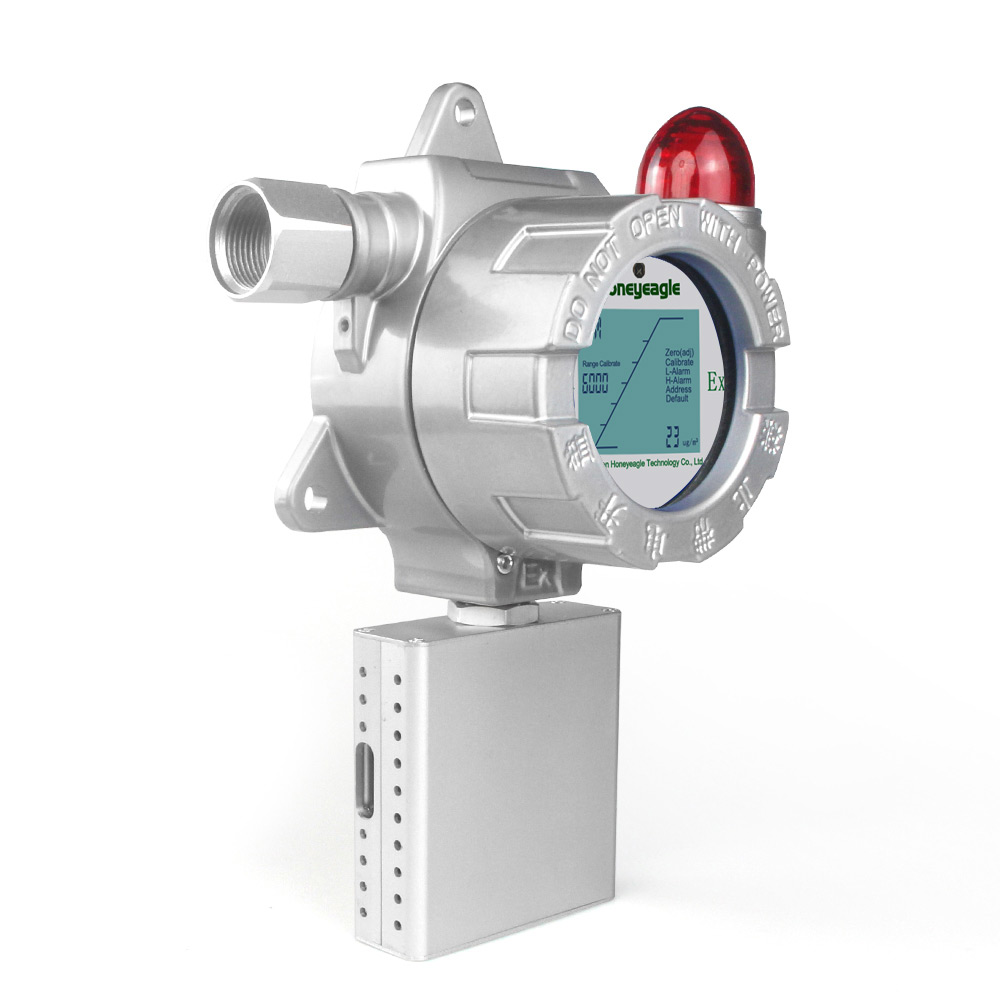
Industrial Fixed Dust Concentration Detector PM Sensor-HNAG1000-PMIndustrial Fixed Dust Concentration Detector PM Sensor
The HNAG1000-PM is an industrial fixed dust detector featuring a high-precision laser scattering sensor. With IP66 protection, explosion-proof casing, and RS485/4-20mA outputs, it ensures real-time, accurate PM monitoring for harsh environments.
Continuous PM Monitor & Explosion-Proof Dust Sensor-HNAG1000-PMContinuous PM Monitor & Explosion-Proof Dust Sensor
Engineered for hazardous industrial sites, the HNAG1000-PM-M provides continuous online particulate matter monitoring. With an IP66 rugged enclosure, ExdIICT6 certification, and seamless PLC integration via RS485/4-20mA, it guarantees absolute safety.
Multi-gas Integrated Pretreatment Online Monitoring System Toxic Gas Analyzer RTO Leak-proof Detection Alarm Instrument-SK/MIC-7500Multi-gas Integrated Pretreatment Online Monitoring System Toxic Gas Analyzer RTO Leak-proof Detection Alarm Instrument
Category: Products Flue gas pretreatment system Simple Pretreatment Online Monitoring System Key words: Products Model: SK/MIC-7500 Measurement object: CO2/Ex/CH4/CO/H2S/O2/N2/NH3/CL2/H2/He/Ar/CH2O/O3/NO/NO2/SO2/C2H4O/PH3/COCL2/HBR/HCL/HCN/CLO2/SIH4/...
Fixed O3 Preprocessing Online Monitoring System-Fixed O3 Preprocessing Online Monitoring System
The HNAG800-O3 Preprocessing Online Monitoring System provides real-time Ozone detection. Featuring an advanced electrochemical sensor in a stainless steel enclosure, it ensures rapid response and high precision for strict industrial safety.
Fixed CLO2 Preprocessing Online Monitoring System-Fixed CLO2 Preprocessing Online Monitoring System
The HNAG800-CLO2 Preprocessing Online Monitoring System delivers real-time Chlorine Dioxide detection. Featuring a highly sensitive electrochemical sensor, it ensures rapid response and high accuracy within a rugged stainless steel enclosure for strict industrial safety.
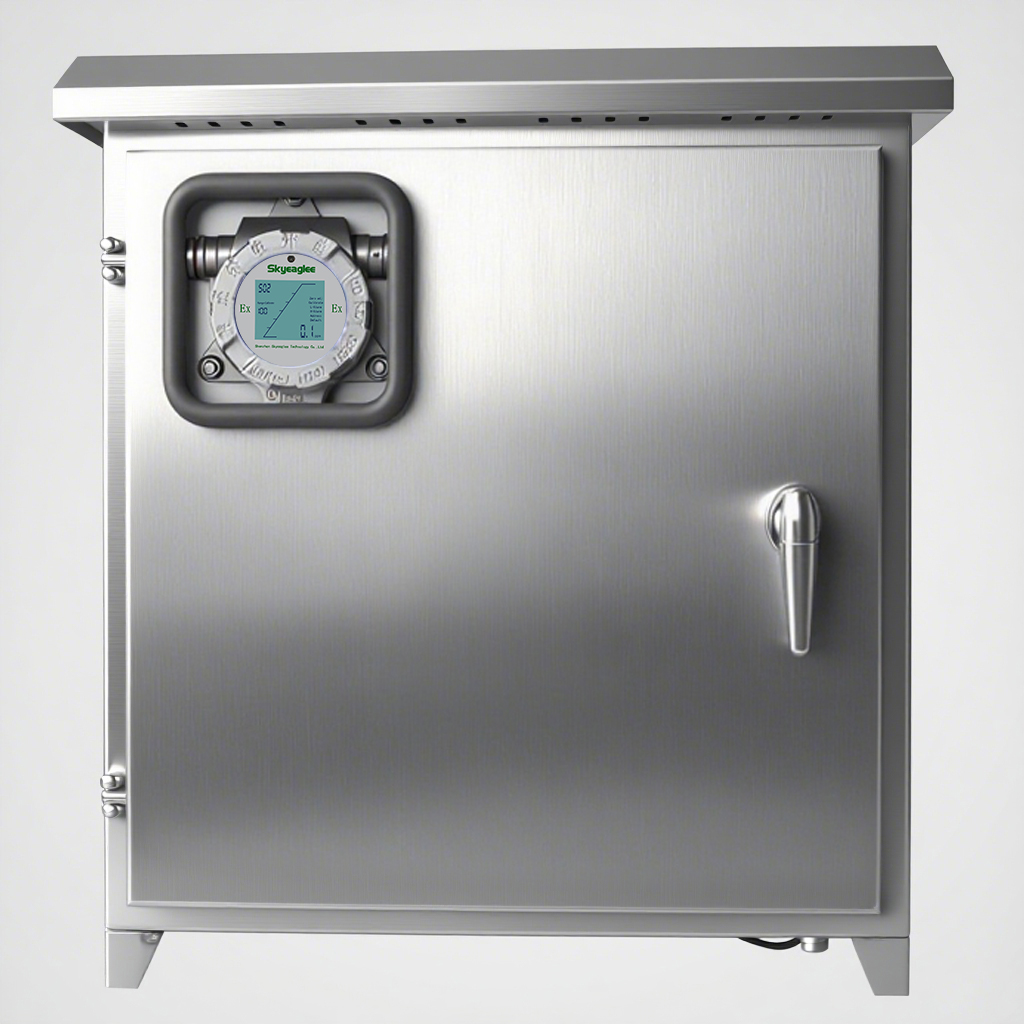
Fixed CL2 Preprocessing Online Monitoring System-Fixed CL2 Preprocessing Online Monitoring System
The HNAG800-CL2 Preprocessing Online Monitoring System delivers real-time Chlorine gas detection. Featuring a highly sensitive electrochemical sensor, it ensures rapid response and high accuracy within a rugged stainless steel enclosure for strict industrial safety.
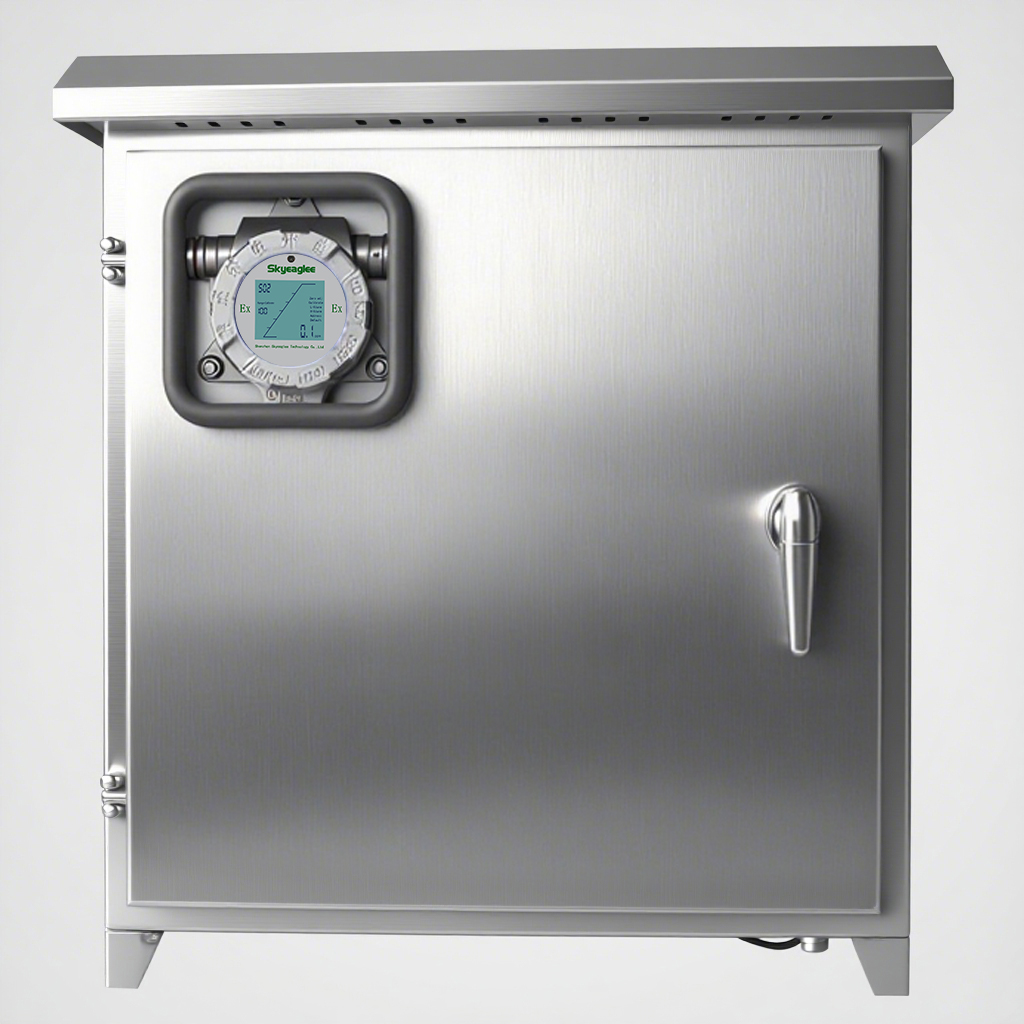
Fixed HF Preprocessing Online Monitoring System-Fixed HF Preprocessing Online Monitoring System
The HNAG800-HF Preprocessing Online Monitoring System delivers real-time Hydrogen Fluoride detection. Featuring a highly sensitive electrochemical sensor, it ensures rapid response and high accuracy within a rugged stainless steel enclosure for robust industrial safety.
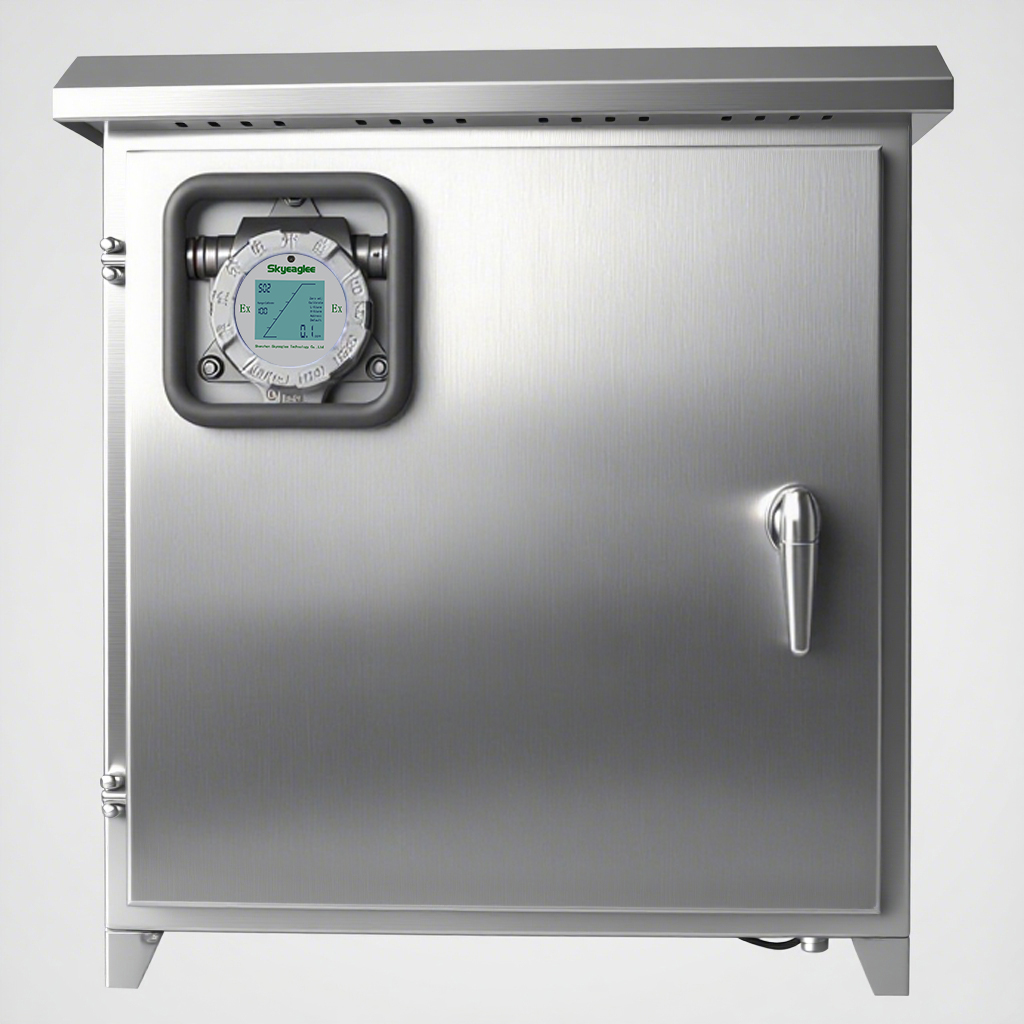
Fixed F2 Preprocessing Online Monitoring System-Fixed F2 Preprocessing Online Monitoring System
The HNAG800-F2 Preprocessing Online Monitoring System provides real-time Fluorine detection. Featuring a precise electrochemical sensor within a robust stainless steel enclosure, it ensures rapid response and high safety in harsh environments.
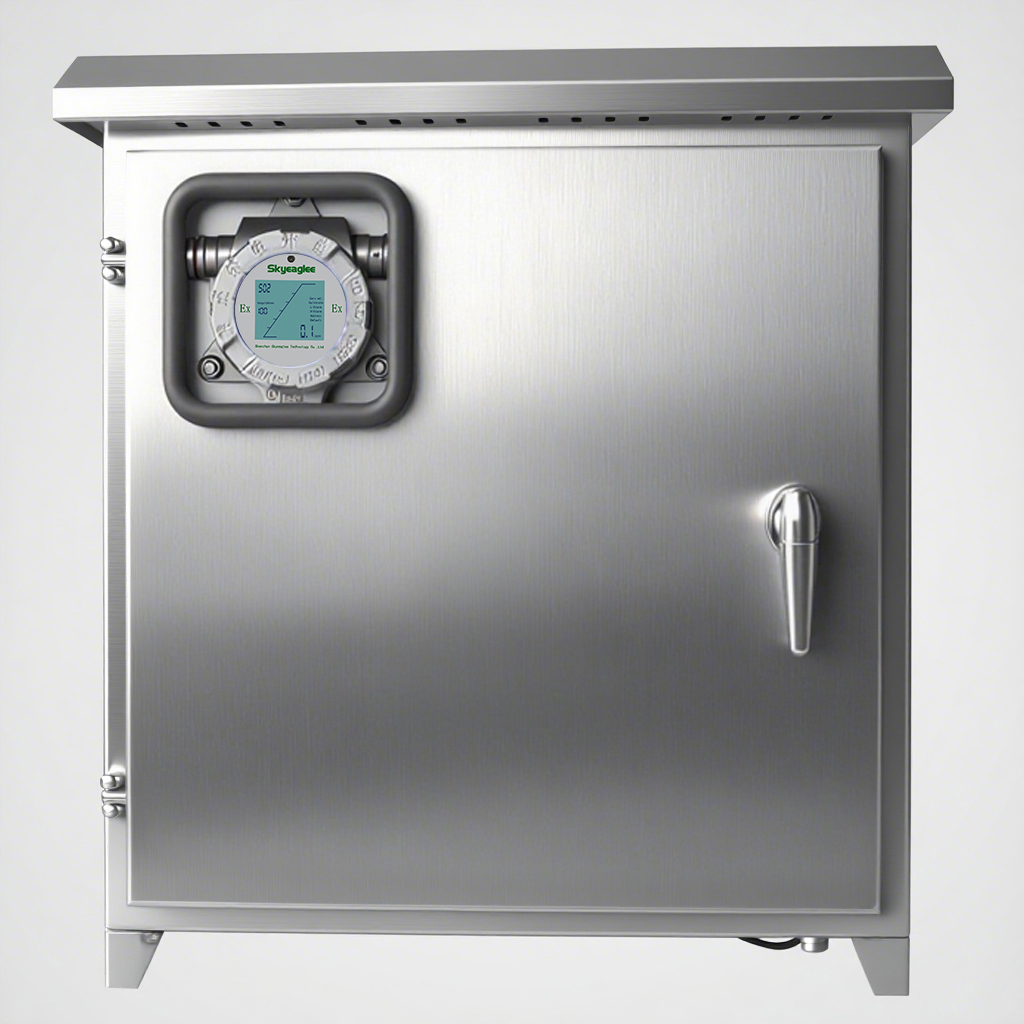
Fixed HBr/HCl Preprocessing Online Monitoring System-Fixed HBr/HCl Preprocessing Online Monitoring System
The HNAG800-HBR/HCL Preprocessing Online Monitoring System provides real-time Hydrogen Bromide and Hydrogen Chloride detection. Featuring a precise electrochemical sensor in a stainless steel enclosure, it ensures rapid response and industrial safety.
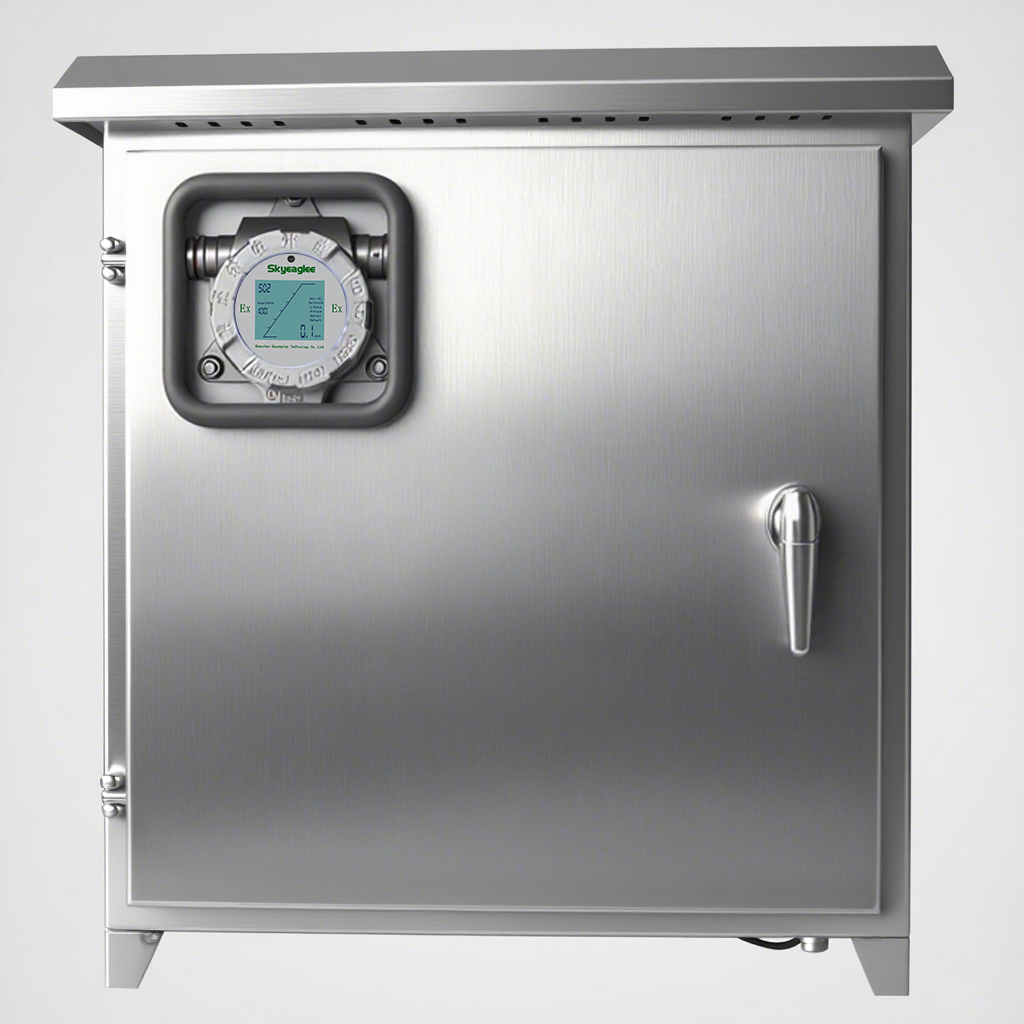
Fixed HCN Preprocessing Online Monitoring System-Fixed HCN Preprocessing Online Monitoring System
The HNAG800-HCN Preprocessing Online Monitoring System delivers real-time Hydrogen Cyanide detection. Featuring a highly sensitive electrochemical sensor, it ensures rapid response, high accuracy, and explosion-proof safety within a rugged stainless steel enclosure.
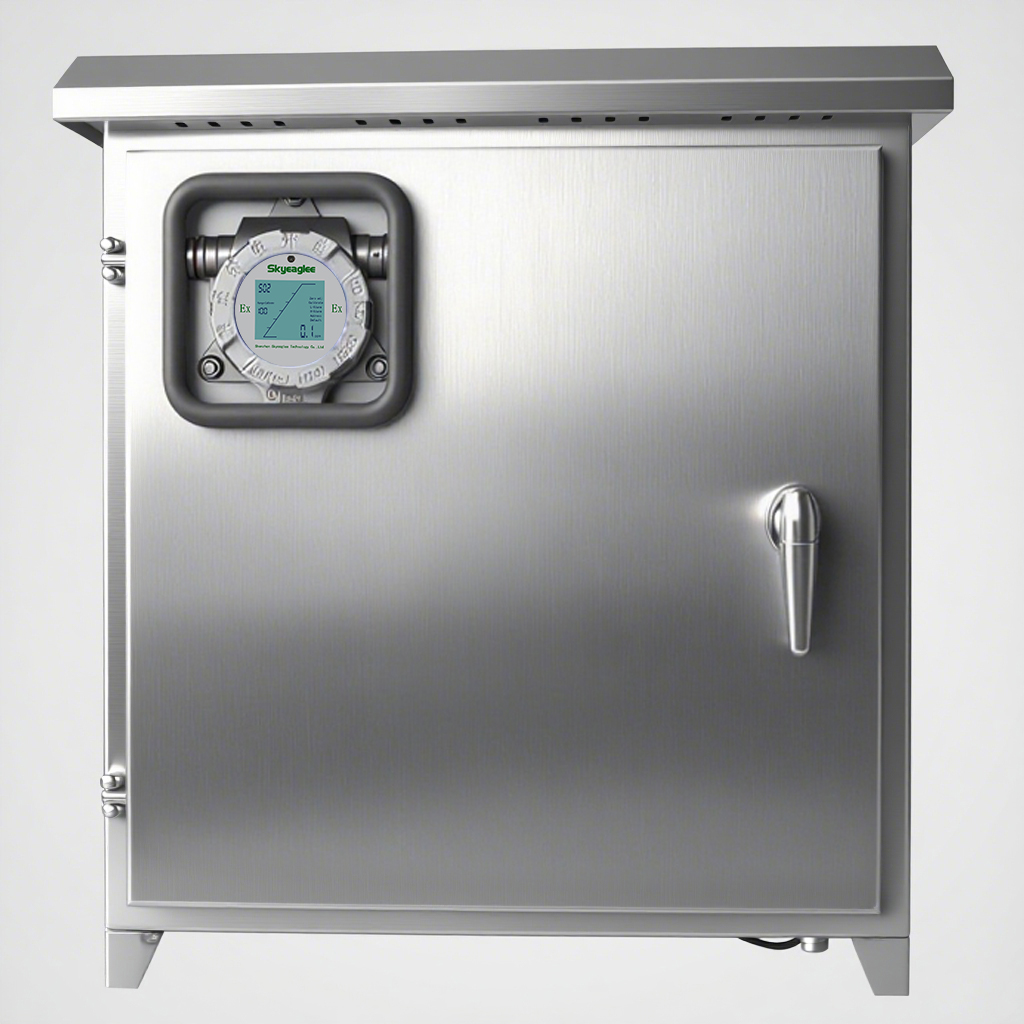
Fixed NO Preprocessing Online Monitoring System-Fixed NO Preprocessing Online Monitoring System
The HNAG800-NO Preprocessing Online Monitoring System delivers real-time Nitric Oxide detection. Featuring an advanced electrochemical sensor for atmospheric monitoring, it ensures rapid response and high precision in a rugged stainless steel enclosure.
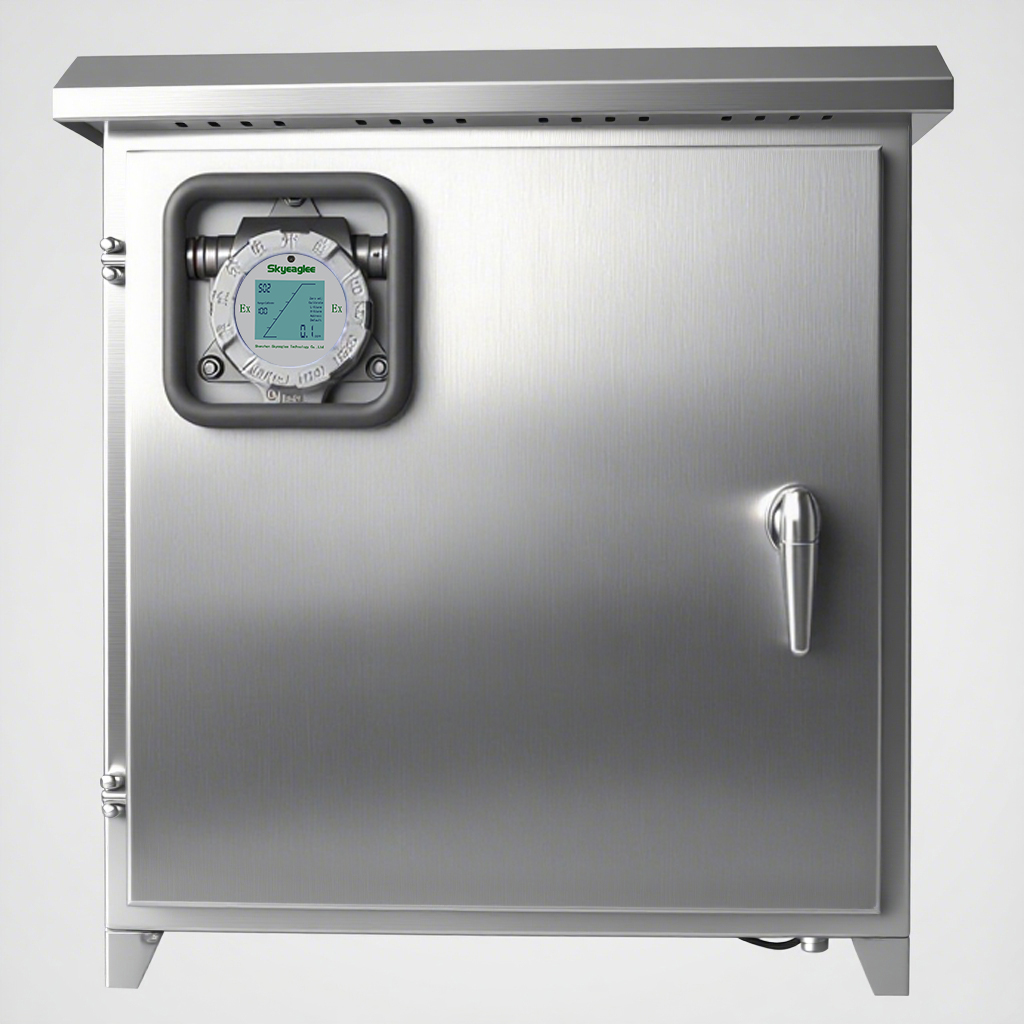
Fixed NH3 Preprocessing Online Monitoring System-Fixed NH3 Preprocessing Online Monitoring System
The HNAG900-NH3 Preprocessing Online Monitoring System delivers real-time, accurate ammonia detection. Engineered with electrochemical and thermal conduction sensors in a robust stainless steel enclosure, it ensures rapid response and safety in harsh industrial environments.
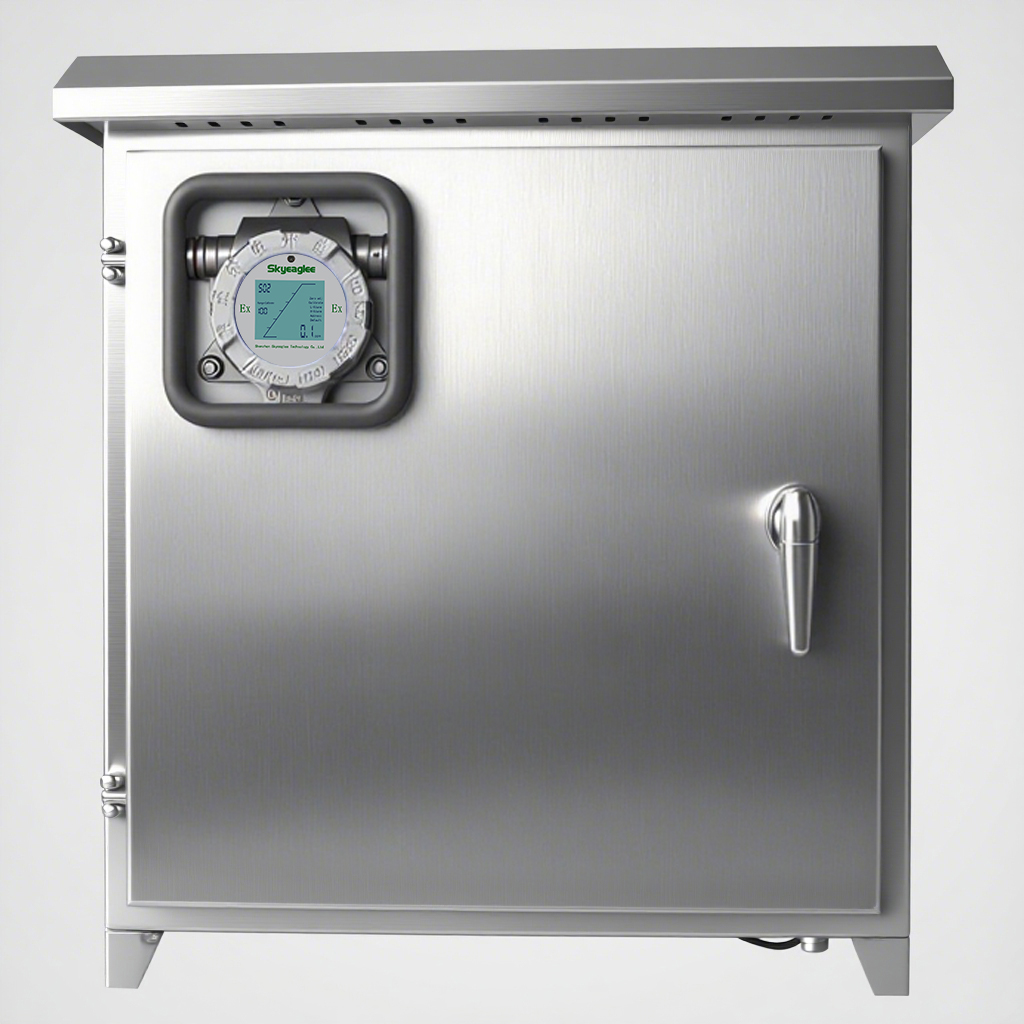
Fixed SO2 Preprocessing Online Monitoring System-Fixed SO2 Preprocessing Online Monitoring System
The HNAG800-SO2 Preprocessing Online Monitoring System delivers real-time Sulfur Dioxide detection. Featuring an advanced electrochemical sensor for flue gas, it ensures rapid response and high precision in a rugged stainless steel enclosure.
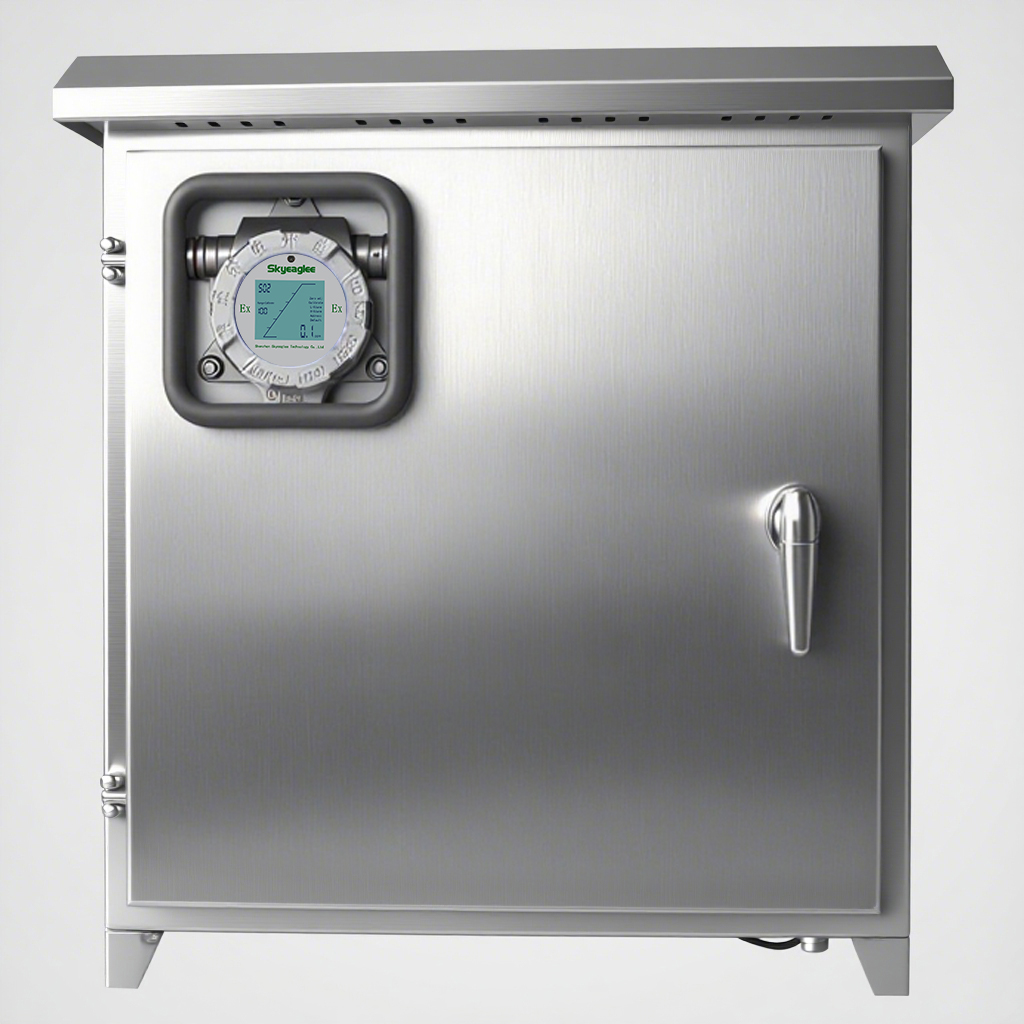
Fixed NO2 Preprocessing Online Monitoring System-Fixed NO2 Preprocessing Online Monitoring System
The HNAG1000-NO2 Preprocessing Online Monitoring System provides real-time Nitrogen Dioxide detection. Engineered with an electrochemical sensor for flue gas applications and housed in robust stainless steel, it guarantees rapid response and industrial safety.
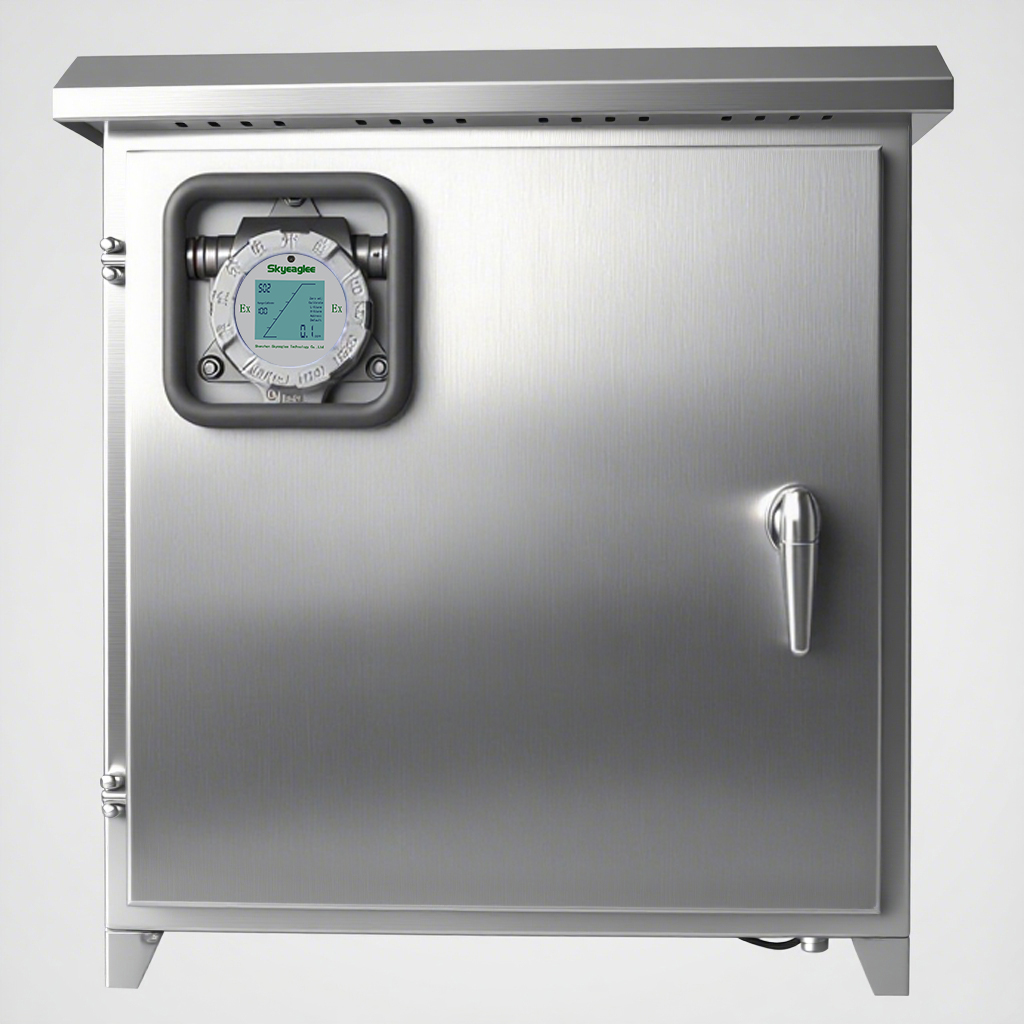
Fixed H2S Preprocessing Online Monitoring System-Fixed H2S Preprocessing Online Monitoring System
The HNAG1000-H2S Preprocessing Online Monitoring System delivers real-time hydrogen sulfide detection. Featuring an advanced electrochemical sensor and a rugged stainless steel enclosure, it ensures rapid response and safety in harsh environments.
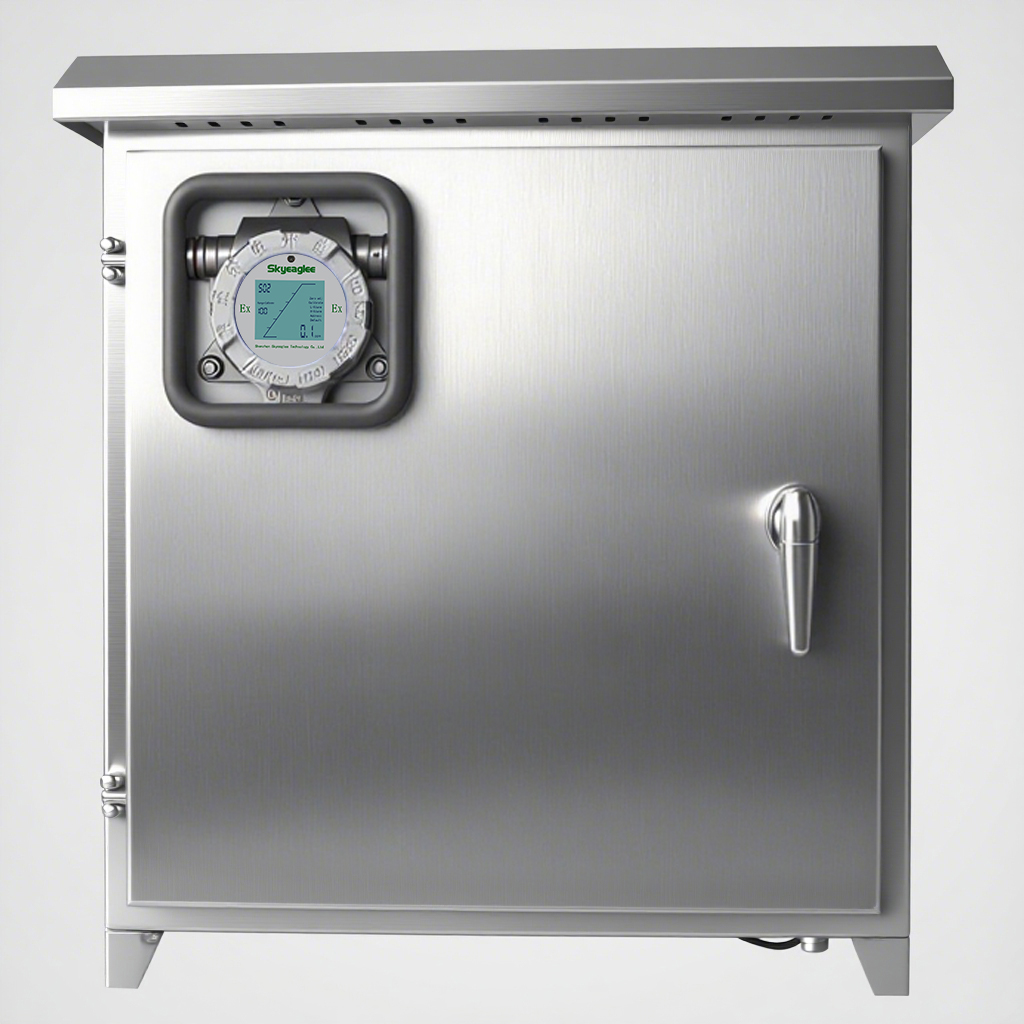
Fixed CFC Gas Preprocessing Online Monitoring System-Fixed CFC Gas Preprocessing Online Monitoring System
The HNAG1000-CFC Preprocessing Online Monitoring System offers continuous, real-time CFC gas detection. Utilizing NDIR and catalytic combustion sensors within a rugged stainless steel enclosure, it ensures high accuracy and safety in harsh environments.
Fixed CO Preprocessing Online Monitoring System-Fixed CO Preprocessing Online Monitoring System
HNAG1000 Fixed CO Preprocessing Monitoring System provides continuous carbon monoxide detection in harsh areas. Built with advanced NDIR sensors and a rugged stainless steel enclosure, it guarantees rapid response, high accuracy, and industrial safety.
HNAG920 Portable NH3 Ammonia Single Gas Detector with Custom Ranges-HNAG920 Portable NH3 Ammonia Single Gas Detector with Custom Ranges
This HNAG920-NH3 handheld single ammonia gas detector provides 12 optional NH3 measuring ranges from 0-10ppm up to 0-100%Vol. It supports auto 180° screen rotation, 4G/WiFi/Bluetooth/LORA wireless transmission, Type-C rechargeable design, 4-side LED alarm lights, durable PC+TPU housing, and allows mobile data viewing & Bluetooth printing for chemical plants, livestock farms and refrigeration workshop hazardous gas monitoring.
Portable Methane Gas Detector Handheld Methane Monitor-HNAG900Portable Methane Gas Detector Handheld Methane Monitor
Skyeaglee HANG-900-CH4-C portable methane gas detector with catalytic detection 0-100%LEL, IP65, Ex ib II CT4 Gb. Expandable to 6 gases, 5400mAh, USB data export. Professional methane gas monitor for oil, coal, petrochemical.
Portable pump-assisted diffusion-type hydrogen gas detector-HNAG920-H2Portable pump-assisted diffusion-type hydrogen gas detector
Explore the Portable pump - assisted diffusion - type hydrogen gas detector. This detector combines pump - assisted and diffusion - type features, offering high - precision hydrogen detection.
Industrial Fixed Dust Concentration Detector PM Sensor-HNAG1000-PMIndustrial Fixed Dust Concentration Detector PM Sensor
The HNAG1000-PM is an industrial fixed dust detector featuring a high-precision laser scattering sensor. With IP66 protection, explosion-proof casing, and RS485/4-20mA outputs, it ensures real-time, accurate PM monitoring for harsh environments.
Continuous PM Monitor & Explosion-Proof Dust Sensor-HNAG1000-PMContinuous PM Monitor & Explosion-Proof Dust Sensor
Engineered for hazardous industrial sites, the HNAG1000-PM-M provides continuous online particulate matter monitoring. With an IP66 rugged enclosure, ExdIICT6 certification, and seamless PLC integration via RS485/4-20mA, it guarantees absolute safety.
Multi-gas Integrated Pretreatment Online Monitoring System Toxic Gas Analyzer RTO Leak-proof Detection Alarm Instrument-SK/MIC-7500Multi-gas Integrated Pretreatment Online Monitoring System Toxic Gas Analyzer RTO Leak-proof Detection Alarm Instrument
Category: Products Flue gas pretreatment system Simple Pretreatment Online Monitoring System Key words: Products Model: SK/MIC-7500 Measurement object: CO2/Ex/CH4/CO/H2S/O2/N2/NH3/CL2/H2/He/Ar/CH2O/O3/NO/NO2/SO2/C2H4O/PH3/COCL2/HBR/HCL/HCN/CLO2/SIH4/...
Fixed O3 Preprocessing Online Monitoring System-Fixed O3 Preprocessing Online Monitoring System
The HNAG800-O3 Preprocessing Online Monitoring System provides real-time Ozone detection. Featuring an advanced electrochemical sensor in a stainless steel enclosure, it ensures rapid response and high precision for strict industrial safety.
Fixed CLO2 Preprocessing Online Monitoring System-Fixed CLO2 Preprocessing Online Monitoring System
The HNAG800-CLO2 Preprocessing Online Monitoring System delivers real-time Chlorine Dioxide detection. Featuring a highly sensitive electrochemical sensor, it ensures rapid response and high accuracy within a rugged stainless steel enclosure for strict industrial safety.
Fixed CL2 Preprocessing Online Monitoring System-Fixed CL2 Preprocessing Online Monitoring System
The HNAG800-CL2 Preprocessing Online Monitoring System delivers real-time Chlorine gas detection. Featuring a highly sensitive electrochemical sensor, it ensures rapid response and high accuracy within a rugged stainless steel enclosure for strict industrial safety.
Fixed HF Preprocessing Online Monitoring System-Fixed HF Preprocessing Online Monitoring System
The HNAG800-HF Preprocessing Online Monitoring System delivers real-time Hydrogen Fluoride detection. Featuring a highly sensitive electrochemical sensor, it ensures rapid response and high accuracy within a rugged stainless steel enclosure for robust industrial safety.
Fixed F2 Preprocessing Online Monitoring System-Fixed F2 Preprocessing Online Monitoring System
The HNAG800-F2 Preprocessing Online Monitoring System provides real-time Fluorine detection. Featuring a precise electrochemical sensor within a robust stainless steel enclosure, it ensures rapid response and high safety in harsh environments.
Fixed HBr/HCl Preprocessing Online Monitoring System-Fixed HBr/HCl Preprocessing Online Monitoring System
The HNAG800-HBR/HCL Preprocessing Online Monitoring System provides real-time Hydrogen Bromide and Hydrogen Chloride detection. Featuring a precise electrochemical sensor in a stainless steel enclosure, it ensures rapid response and industrial safety.
Fixed HCN Preprocessing Online Monitoring System-Fixed HCN Preprocessing Online Monitoring System
The HNAG800-HCN Preprocessing Online Monitoring System delivers real-time Hydrogen Cyanide detection. Featuring a highly sensitive electrochemical sensor, it ensures rapid response, high accuracy, and explosion-proof safety within a rugged stainless steel enclosure.
Give us a free quote
Submit this form and our sales representative will contact you soon.
Contact Us


Fill out the form